Custom Hoodie Manufacturing 101: A Hoodie Manufacturer's Guide
Custom Hoodie Manufacturing 101: What a Hoodie Manufacturer Actually Controls
Most "hoodie 101" content online is just a spec sheet that stops after listing grams-per-square-meter numbers. But what actually decides whether a customer keeps the garment or returns it comes down to three decisions: fabric weight, loop-back versus fleece-back knit structure, and a set of hidden details we call the "handfeel tax." When you run custom hoodies, you lock the weight range first (280–450 GSM, with 380–450 for heavyweight streetwear), then the back-face structure (French terry or brushed fleece), and only then write the hood, pocket, and rib details that the hand feels immediately into the tech pack. Get the order wrong and your sampling rounds and lead time pay for it.
- 01Custom Hoodie Manufacturing 101: only three real decisions
- 02A real pitfall: the "250 GSM saves cost" heavyweight line that failed
- 03Fabric weight: how to pick inside 280–450 GSM, and how to pin the tolerance
- 04Knit structure: the back face matters more than the front
- 05The handfeel tax: four hidden line items that never appear on a spec sheet
- 06Three weight tiers and where each one positions you
- 07Proto verification: four things you must feel in hand
- 08From material selection to bulk in 5 steps
- 09Common questions
A hoodie is not "a pair of sweatpants with a hood attached." It is a stack of small material decisions: yarn count, loop structure, weight tolerance, drawcord thickness, rib recovery. And the customer's hand reads every one of those decisions in the first ten seconds of picking it up. A spec sheet will not make those decisions for you, but your return rate will honestly settle them.
This guide is written for growing brands planning a custom hoodie line. No fluff. We cover only the three layers of decisions that actually move the finished product on a real factory floor, and the single easiest place to go vague at each layer.
A Real Pitfall: The "250 GSM Saves Cost" Heavyweight Line That Failed
Start with a generalized cautionary case. A growing streetwear brand launched its first collection wanting a "heavyweight, premium-feel hoodie." During quoting, one factory suggested dropping the fabric from 400 GSM to 250 GSM, arguing "it looks about the same, saves you thirty percent on material." The brand placed 300 units of bulk production without running a wash test.
When goods hit the warehouse, the problems surfaced all at once: light-colored styles showed show-through under backlight, revealing the print on the inside; after one wash the silhouette loosened, dropped shoulders became slumped shoulders; cuff ribs lost recovery and bunched at the wrist after two wears. The most brutal review read "feels like discount-store thermal underwear." That batch was finally cleared at 30% off, and the repeat-purchase data for the launch collection was destroyed with it. A customer never gives you a second first impression.
That factory did not lie. 250 GSM genuinely saves material cost. But it optimized the factory's margin, not your product. Weight is not a cost line; it is a positioning line. The price you sell at and the handfeel the customer expects determine which weight tier you should land in. Once positioning is set, fabric cost is a deduction, not a negotiation.
Fabric Weight: How to Pick Inside 280–450 GSM, and How to Pin the Tolerance
Weight (GSM, grams per square meter) is the most watched and the most misunderstood number on a hoodie. The conclusion first: a proper custom hoodie runs 280–450 GSM, with the heavyweight streetwear sweet spot at 380–450.
Below 280: what you save in fabric you lose in shape
Hoodies under 280 GSM show through when held to light as a single layer. The bigger problem is wash performance: light terry cloth cannot survive repeated laundering. Yarn shift, placket twist, hem flip; after three washes it essentially says goodbye to the word "silhouette." If you run a base-layer line, this range works. For an outward-facing hoodie line, we do not recommend dropping below 320.
380–450: the heavyweight sweet spot
380 GSM double-yarn terry is our standard stock for streetwear brands. Thick without being stiff, it keeps its drape, and its face holds both heavy-screen and water-based prints. Pushing past 450 GSM, wrinkle resistance and shape memory peak, but so does the garment's total weight. Summer and southern-hemisphere markets need caution. Pile it up to 500 and fewer people wear it, fewer still buy it. That is building a display piece, not a product.
Tolerance: without ±5%, the weight number is not written at all
Every fabric has dye-lot variation, so the weight on a tech pack must carry a tolerance. The industry standard is ±5%. The correct way to write 380 GSM is "380 GSM ±5% (361–399)." A weight promise without tolerance lets the factory split the middle. When your goods arrive at 355 and the order says 380, you have zero basis for a dispute. We weigh every dye lot on intake and re-test before bulk cutting. Any lot out of range goes back whole. That is the precondition that lets a tech pack actually "lock" anything.
Weight decides the customer's first handfeel. Knit structure decides how it feels after three washes. The first decides whether they put it on. The second decides whether they come back.
Knit Structure: The Back Face Matters More Than the Front
Almost no one explains this layer properly: a hoodie's back face decides its product character, and it sits closer to a brand-positioning decision than the front does. The front face of hoodie fabric all looks about the same. Every distinction lives on the back.
French Terry (loop back)
The back is dense small loops: clean structure, moisture-wicking and breathable, with a crisp drape. It gives the hoodie "structure": the silhouette holds, shoulder lines stay sharp, and it layers without bulk. For structured streetwear, all-over prints, and year-round basics, French terry is the safe answer. The trade-off: it is not plush. Customers chasing a "cloud-wrap" feel will find it not soft enough.
Brushed / Fleece-back
The back is raised and napped: fluffy, skin-touching, heat-retaining. This is the source of "lounge feel" and "warmth feel." But the two-sided nature of a napped structure is equally honest: higher pilling probability, elbows and knees slacken more easily, and at equal weight it breathes worse than terry. For autumn-winter warmth lines and lounge scenarios, brushed fleece is the right call.
We have watched two nearly identical-spec hoodie lines split a market clean in half purely on loop-back versus brushed-back: one reads "premium studio," the other reads "lounge." Hard rule: decide the back face before the color. Any factory can match a Pantone number. A back face that pills after three washes, no factory can rescue for you. Get the knit structure right and color is the easiest step.
The Handfeel Tax: Four Hidden Line Items That Never Appear on a Spec Sheet
This is a concept I walk every new brand through. Two hoodies can share the same weight, same cotton, same color. One feels cheap in hand, the other premium. The gap is the "handfeel tax": a set of details that never land on a spec sheet yet live entirely in the customer's hand. These four usually collect it:
One, yarn grade. At the same 380 GSM, combed cotton and carded cotton differ by a full price tier in handfeel. Combed yarn has fewer surface hairs, a cleaner cloth face, and markedly less pilling after washing. The few dollars per kilo a low-grade yarn saves all convert into that half-second of "cheap" when the customer picks it up.
Two, loop tension. Uneven loop tension during knitting leaves a faint "cloud mottle" on the cloth face and a floaty drape. This defect may not even show under studio lighting, but a light shake in the hand tells you the cloth is "not solid." It cannot be fixed later; only the knitting mill's machine level controls it. This is exactly why our fabric comes from designated knit mills, never open-market spot goods.
Three, drawcord and hardware. The drawcord's thickness, weave density, and the metal or molded tip at the end are the first detail the customer fiddles with. A thin, flat cord that curls the moment you pull it can wipe out the premium feel that 400 GSM of heavyweight fabric built in one move. The drawcord weight should meet or exceed the perceived expectation set by the fabric weight. It sounds mystical, but anyone who has felt both understands in a second.
Four, rib recovery. The elastane content and stitch density of the cuff and hem ribs decide recovery. Poor ribs "open up" after two wears and bunch at the wrist and ankle. Our ribs are ordered separately from the body as 2×2 high-recovery rib, with elastane content and stitch count written into the tech pack, and recovery-tested at the proto stage.
No single item of the handfeel tax is fatal, but together they decide that half-second of "worth the price." A transparent manufacturing partner lets you feel the real thing before bulk: fabric swatches, the actual hood structure, rib recovery samples, not renderings.
Three Weight Tiers and Where Each One Positions You
Compress the three decision layers above into one selection table. Before placing a custom hoodie order, first find your seat among these three tiers:
| Dimension | Light 280–320 GSM | Heavy 380–450 GSM (sweet spot) | Super-heavy 450 GSM+ |
|---|---|---|---|
| Best for | Layering base, spring-fall light, body-fit lines | Streetwear main line, year-round, brand flagship | Autumn-winter limited, oversized concept |
| Recommended back | Mostly French terry | Terry or fleece, pick one by positioning | Mostly brushed fleece, warmth first |
| Post-wash stability | Demands extreme shape control, easily sags | Stable, holds silhouette well | Most stable, but heavy to wear |
| Print fit | Water-based, direct-to-garment | Heavy-screen, water-based, embroidery all fit | Heavy-screen, applique |
| Per-piece fabric cost | Low | Mid-high | Highest |
| Complaint risk | Show-through, post-wash sag | Almost none, watch southern summers | Weight puts buyers off, summer stall |
For a growing brand's first hoodie line, we usually recommend landing straight in the 380–450 tier. It is the threshold where "the customer feels it's worth it in hand," and also the tier least likely to be price-shopped on reorders. Leave the light tier for phase two, once you have stabilized and need to fill out the price band.
Proto Verification: Four Things You Must Feel in Hand
Paper specs can be discussed; handfeel must be verified on a physical sample. In the proto stage of a custom hoodie (our first sample runs 7–10 working days, with an in-house pattern room, nothing outsourced), you should demand these four physical items from the factory:
One, a fabric swatch that includes a post-wash sample. Looking only at the greige swatch is not enough. Require the factory to provide the same-weight cloth "after one wash," so you can read shrinkage, pilling, and handfeel change. Shrinkage data must flow back into the pattern: 380 GSM terry commonly runs 3–4% warp shrinkage, so the pattern chest must be opened to about 114 cm to land a 110 cm finished chest, or the bulk goods come up short after washing.
Two, the actual hood structure. Three-panel or two-panel hood, whether the hood has a reinforcement lining, whether the drawcord eyelets are metal grommets or directly bound buttonholes, whether the double-needle stitching lies flat. These decide whether the hood "stands up." A soft, collapsed hood is a minus on the shelf, and it is exactly the part a rendering can never show.
Three, the pocket and stress points. The pocket of a hoodie is a load-bearing zone: the two ends of the opening, the pocket-mouth stitching, the junction with the hem rib, all need to show reinforced stitching. At the proto stage, stretch the pocket mouth with your hand. After bulk, the customer's phone and hands will stress it more realistically than your QC simulation.
Four, a rib recovery sample. Stretch the cuff to maximum, release three times, and watch return speed and residual deformation. Ribs are the dividing line between "worn one season" and "worn three seasons," and the touchstone for whether a factory is willing to spend on the small things.
Only after the sample clears these four gates do you talk bulk. Time saved in the sampling rounds is repaid double in lead time and rework during bulk. It is one of the most stable laws from twelve years inside a dual-factory system.
From Material Selection to Bulk in 5 Steps
Collapse the whole guide into one executable order. A custom hoodie from zero to bulk, on this rhythm, takes the fewest wrong turns:
- Decide the back face before the color: French terry or brushed fleece is a brand-positioning decision that precedes all color discussion. If unsure, have both cloths made as handfeel samples and compare on body.
- Land the weight with tolerance: seat within 280–450 (first drop recommended 380–450), and write the tech pack as "380 GSM ±5%" so there is no room to argue.
- Clear the handfeel tax item by item: yarn grade (combed or carded), drawcord spec, rib elastane and stitch count, loop tension. Write all four into the tech pack; miss one and you miss a stretch of handfeel.
- Verify the four physical samples: post-wash cloth, hood structure, pocket stress, rib recovery. Feel all of them in hand before sealing the sample. Flow shrinkage data back into the pattern.
- Lock the sample and the dye lot for bulk: keep a sealed sample on file, weigh every dye lot, run AQL 1.5 with an 8-step inspection, and produce reorders against the retained sample. Second order matches first, and the brand earns the word "silhouette."
Common Questions
Is the difference between 380 GSM and 450 GSM large, and how should a first drop choose?
The in-hand difference is clear: 450 is thicker and wrinkles less, but the whole garment is heavier, and it runs heavy in summer and southern markets. For a first drop we recommend landing at 380–420 GSM. It is the threshold where "it feels premium in hand," it wears year-round, and it has the most reorder elasticity. Reserve 450-plus for autumn-winter limited runs.
Is French terry not warm enough?
Depends on the scenario. Terry insulates worse than brushed fleece but breathes and drapes better, so it is actually more comfortable for spring-autumn and layering. For genuine deep-winter styles, 450 GSM-plus brushed fleece or a bonded sherpa lining fits better. When warmth and structure trade off, streetwear brands mostly choose structure.
With a ±5% weight tolerance, will arrivals get "legally shrunk"?
Tolerance runs both ways: writing ±5% means falling below the lower limit is equally a breach. Our practice is to weigh every lot on intake and re-test before cutting; any lot out of range goes back whole. Inspection samples weight under AQL 1.5. What you watch is not whether a tolerance exists, but whether the factory records every lot.
How many sampling rounds are enough, and will it delay the lead time?
Normally two rounds: the first for silhouette and fabric handfeel, the second to confirm details (hood, pocket, rib). Each round is 7–10 working days. More important than the number of rounds is the completeness of feedback in each. Raise all four physical-sample issues at once, and it moves far faster than three rounds each carrying one issue.
Is pilling on brushed fleece unsolvable?
Controllable but not eradicated. Three levers: combed yarn as the base, anti-pilling setting after napping, and a care label that states the wash condition clearly (wash inside out, tumble dry low). Hit all three and brushed fleece's pilling within three washes lands at "acceptable." Miss any one and it will pill within three washes, guaranteed.
How do I ensure the fabric matches the first order on reorders?
Three things: keep a sealed sample on file (fabric swatch plus sample garment, one of each), record the yarn lot and dye-lot numbers, and produce reorders against the retained sample with weight re-test. Changing lots carries color-shift risk, so we hold margin by lot on bulk orders, and reorders preferentially use the same recorded yarn lot.
About the Production Line
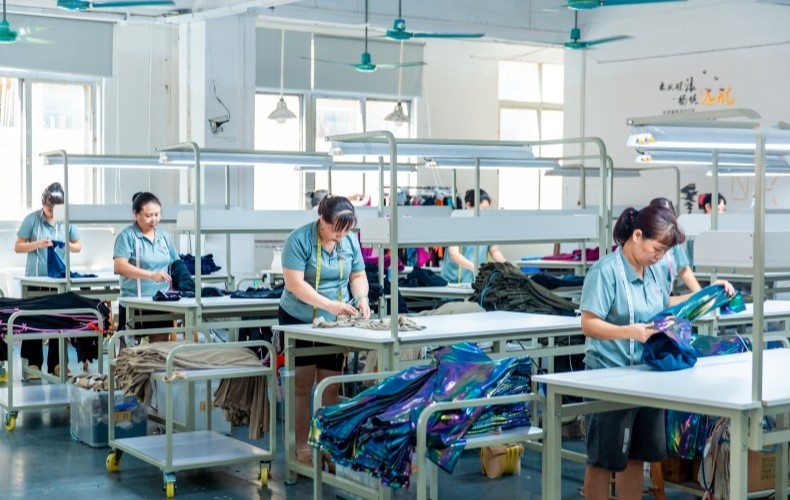
Two plants in Guangxi and Dongguan, totaling 20,000 square meters with 500,000 pieces monthly capacity, running streetwear OEM / ODM since 2014 and serving over 1,200 brands. Fabric comes from designated knit mills, weighed per lot. Quality runs AQL 1.5 with an 8-step process, certified BSCI (Grade B), GRS, ISO 9001, OEKO-TEX Standard 100. Shipment port is Shenzhen (FOB Shenzhen).
Ready to plan your custom hoodie line? Send your target weight, back-face preference (terry or fleece), and a reference style. Before sampling we mail you fabric swatches and the actual hood structure, so the four handfeel-tax items get confirmed sample by sample before bulk. 380–450 GSM double-yarn terry is standard stock; first sample in 7–10 days.